2026年4月12日星期日

Injection Molding Sink Marks: Causes, Prevention, and Real Factory Solutions

 Sink marks are one of the most common quality problems in plastic injection molding. These small surface depressions may look minor at first glance, but they can seriously affect the appearance and performance of a product.

For manufacturers producing consumer electronics, automotive components, or medical devices, even small sink marks can lead to product rejection or customer complaints.

At CNMOULDING (Shanghai), a plastic injection mold manufacturer established in 1997, we frequently help customers solve molding defects during product development and mass production. With more than 25 years of experience in mold manufacturing and injection molding services, we have encountered many sink mark issues across different industries.

In this article, we explain what sink marks are, why they occur, and how they can be prevented, along with a real case study from our factory.
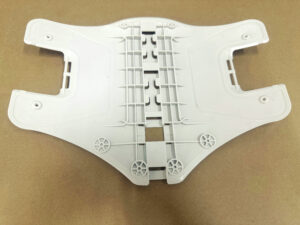
What Are Sink Marks in Injection Molding

Sink marks are small depressions or dimples that appear on the surface of molded plastic parts. They typically occur in thicker areas of the part where the material cools unevenly.

These defects usually appear:

  • near ribs

  • around screw bosses

  • in thick wall sections

  • close to structural supports

Sink marks are caused by plastic shrinkage during the cooling process.

When molten plastic cools inside the mold cavity, it shrinks. If the outer surface of the part cools faster than the inner material, the internal shrinkage pulls the surface inward, creating a visible depression.

While sink marks are often cosmetic defects, they can also indicate structural design problems in the part or mold.

Why Sink Marks Occur in Injection Molding

Several factors can cause sink marks during injection molding production.

Understanding these causes is the first step toward solving the problem.

1 Uneven Wall Thickness

One of the most common causes of sink marks is uneven wall thickness.

When a plastic part contains thick sections next to thin sections, cooling occurs at different speeds. Thick areas remain hot longer, and the material inside continues to shrink while the outer surface has already hardened.

This internal shrinkage pulls the surface inward, forming sink marks.

Engineering Recommendation

Product designers should aim for uniform wall thickness whenever possible. If thicker structural areas are necessary, techniques such as coring or rib design optimization should be used.


2 Improper Rib or Boss Design

Ribs and screw bosses are often required to strengthen plastic parts, but poor design can easily cause sink marks.

If a rib or boss is too thick compared to the main wall thickness, the additional material increases shrinkage during cooling.

A common guideline used by mold designers is:

  • rib thickness should be 50%–70% of the main wall thickness

Following this rule helps reduce the risk of visible sink marks on the surface.

3 Insufficient Packing Pressure

After the mold cavity is filled, holding pressure (packing pressure) is applied to compensate for material shrinkage during cooling.

If packing pressure is too low or holding time is too short, there will not be enough material to compensate for shrinkage.

As a result, sink marks may appear on the surface of the molded part.

Solution

Optimizing holding pressure and holding time can significantly reduce sink marks in many cases.
4 Poor Mold Cooling Design

Cooling is one of the most critical factors in injection molding.

If cooling channels are poorly designed, some areas of the mold may cool much slower than others.

This uneven cooling creates differential shrinkage and increases the likelihood of sink marks.

Solution

Proper cooling channel design ensures uniform temperature distribution across the mold cavity.

In many modern projects, conformal cooling design or optimized cooling circuits are used to improve cooling efficiency.

Real Case Study: Consumer Electronics Housing

One of our customers, a consumer electronics manufacturer from North America, contacted us regarding a sink mark issue on a plastic housing component.

The part was designed for a smart home device and required excellent cosmetic quality because it was visible to end users.

Project Details

  • material: ABS

  • wall thickness: 2.0 mm

  • part type: electronic housing

  • annual production volume: 1.8 million units

Problem Description

During trial production, visible sink marks appeared around several screw bosses on the outer surface of the housing.

Although the defect did not affect product functionality, it failed the customer’s visual quality requirements.

Engineering Analysis

Our engineering team conducted a full DFM (Design for Manufacturing) analysis and Moldflow simulation.

The analysis revealed two major issues:

  1. The screw boss thickness was 3.2 mm, which was significantly thicker than the surrounding wall thickness.

  2. The cooling channels near the boss area were not optimized.

These two factors caused uneven cooling and excessive shrinkage near the boss structures.

Our Engineering Solution

To solve the problem, our engineers implemented several improvements.

1 Boss Coring Optimization

We modified the screw boss design by adding internal coring to reduce material thickness.

This adjustment maintained structural strength while reducing shrinkage risk.

2 Cooling System Optimization

Additional cooling channels were added near the critical area to improve heat removal during the cooling stage.

3 Process Parameter Adjustment

Injection molding parameters were optimized, including:

  • increased holding pressure

  • extended holding time

  • adjusted melt temperature

Final Results

After implementing these changes, the results were significantly improved.

  • sink marks were completely eliminated

  • surface quality met customer cosmetic standards

  • cycle time was reduced by 6 seconds

The customer successfully moved into mass production and later partnered with us on additional mold projects.

Best Practices to Prevent Sink Marks

Based on our experience from hundreds of injection molding projects, preventing sink marks requires collaboration between product designers, mold designers, and process engineers.

Key recommendations include:

Maintain Uniform Wall Thickness

Consistent wall thickness helps ensure uniform cooling and reduces shrinkage differences.

Optimize Rib and Boss Design

Following proper design guidelines prevents excessive material buildup in localized areas.

Use Moldflow Simulation

Simulation software can predict shrinkage behavior before the mold is manufactured.

Improve Cooling Channel Layout

Efficient cooling design ensures even temperature distribution across the mold.

Optimize Injection Molding Parameters

Proper packing pressure and holding time help compensate for material shrinkage.

Why Work With an Experienced Mold Manufacturer

Sink marks may appear simple, but solving them often requires deep experience in mold design, material behavior, and injection molding processes.

At CNMOULDING (Shanghai), we combine decades of engineering expertise with modern manufacturing technology.

Our capabilities include:

  • precision injection mold manufacturing

  • injection molding production

  • DFM and mold design optimization

  • defect analysis and troubleshooting

Our company operates under ISO9001 quality management standards and ISO13485 certification for medical device manufacturing, ensuring consistent quality and strict production control.

Need Help Solving Injection Molding Defects?

If your project is experiencing sink marks, warpage, flash, or other molding defects, our engineering team can help analyze the problem and provide practical solutions.

With more than 25 years of mold manufacturing experience, CNMOULDING supports customers worldwide with reliable tooling and production services.

Contact our Shanghai engineering team today to discuss your project and receive professional support.

2026年4月7日星期二

How Much Does a Plastic Injection Mold Cost?


One of the most common questions product developers ask when starting a manufacturing project is:

How much does an injection mold cost?

The cost of a plastic injection mold can vary widely depending on part complexity, mold size, material requirements, and production volume. Some molds may cost only a few thousand dollars, while complex molds for automotive or medical applications can exceed $50,000 or more.

Understanding the factors that affect injection mold cost can help companies better plan their manufacturing budget and avoid unnecessary expenses during product development.

At CNMOULDING, a Shanghai-based mold manufacturer established in 1997, we have produced hundreds of plastic injection molds for global customers in automotive, electronics, and medical industries. Through years of mold design and manufacturing experience, we have seen how smart engineering decisions can significantly reduce tooling costs.

In this guide, we explain typical injection mold price ranges and the key factors that influence mold manufacturing cost.

Typical Injection Mold Cost Range

Injection mold costs vary depending on mold complexity and production requirements. The following ranges reflect common pricing in the manufacturing industry.

Prototype Mold

Typical cost:

$1,000 – $5,000

Prototype molds are designed for product testing or small production runs. These molds often use simplified structures and may be made from aluminum or softer mold steels.

They allow companies to verify product design before investing in a full production mold.

Standard Production Mold

Typical cost:

$5,000 – $30,000

This is the most common mold type used for consumer products and industrial components.

Production molds are usually made from durable steel materials such as P20 or H13 and are designed for long-term manufacturing.

High-Precision or Multi-Cavity Mold

Typical cost:

$30,000 – $100,000+

Complex molds may include multiple cavities, sliding mechanisms, or high precision requirements.

These molds are often used in industries such as:

  • automotive components

  • medical devices

  • electronics housings

Although the initial investment is higher, multi-cavity molds can significantly reduce per-part production costs.

6 Key Factors That Affect Injection Mold Cost

Several engineering factors determine the final cost of an injection mold.

1 Part Complexity

The geometry of the plastic part has the biggest impact on mold cost.

Features that increase mold complexity include:

  • undercuts

  • side holes

  • complex ribs

  • tight tolerances

These features often require additional mold mechanisms such as sliders or lifters, which increase both design and manufacturing time.

2 Mold Size

Larger plastic parts require larger molds and larger injection molding machines.

A bigger mold means:

  • more steel material

  • longer machining time

  • more complex assembly

As mold size increases, manufacturing cost rises accordingly.

3 Mold Steel Selection

The type of steel used in mold manufacturing significantly affects tooling cost and mold durability.

Common mold steels include:

Steel TypeTypical Use
P20General production molds
H13High-temperature or abrasive materials
S136Medical or high-polish applications

Higher-grade steels increase tooling cost but extend mold life and improve product quality.

4 Number of Cavities

Multi-cavity molds allow manufacturers to produce several parts in one injection cycle.

Advantages include:

  • higher production efficiency

  • lower per-part cost

However, increasing cavity numbers also increases mold complexity and tooling cost.

5 Surface Finish Requirements

Products that require high cosmetic quality—such as consumer electronics housings—often need mirror polishing or textured surfaces.

These finishing processes require additional machining and polishing work, increasing mold manufacturing cost.

6 Production Volume

Production volume strongly influences mold design decisions.

For example:

  • small production runs may use simpler molds

  • high-volume production requires stronger mold materials and more robust structures

Choosing the right mold structure for the expected production volume helps optimize tooling investment.

Real Case Study: Automotive Connector Mold

A European automotive supplier contacted our Shanghai engineering team to develop an injection mold for a PA66 glass-fiber reinforced connector housing.

Project Requirements

Material: PA66 GF30
Production volume: 600,000 parts per year
Tolerance requirement: high precision

Initial Cost Estimate

The customer initially planned to use a standard mold design with P20 steel.

Estimated tooling cost:

$22,000

However, because the material contained glass fiber reinforcement, mold wear would likely occur quickly with P20 steel.

Engineering Optimization

Our engineering team recommended several improvements:

  • upgrading the mold steel to H13

  • optimizing gate design for balanced filling

  • improving cooling channel layout

Although these upgrades increased the initial tooling cost slightly, they significantly improved mold durability.

Final Results

The final mold cost was approximately $27,000, but the mold life increased dramatically and production stability improved.

The mold successfully produced over 500,000 parts with minimal maintenance.

In the long term, the customer saved significant costs by avoiding frequent mold repairs and production downtime.

How to Reduce Injection Mold Cost

Companies can reduce tooling costs by optimizing product design and manufacturing strategy.

Some effective methods include:

Simplify Part Design

Reducing unnecessary undercuts or complex features lowers mold complexity.

Maintain Uniform Wall Thickness

Uniform wall thickness improves molding stability and reduces the need for complex mold structures.

Use DFM Analysis Early

Design for Manufacturing analysis helps identify potential problems before mold production begins.

Choose the Right Mold Steel

Selecting the appropriate steel based on production volume helps balance tooling cost and mold durability.

Why Work With an Experienced Mold Manufacturer

Injection mold manufacturing requires specialized engineering expertise. An experienced mold manufacturer can help optimize mold design, reduce production risks, and ensure stable mass production.

At CNMOULDING, our Shanghai factory provides complete services including:

  • injection mold design

  • mold manufacturing

  • plastic injection molding production

  • mold testing and quality inspection

Our facility operates under strict quality systems including:

  • ISO9001 certification

  • ISO13485 certification for medical device manufacturing

With more than 25 years of experience, we support global customers with reliable mold manufacturing solutions.

Start Your Injection Mold Project

If you are planning a new plastic product and want to estimate injection mold cost, our engineering team can review your design and provide professional recommendations.

Contact our Shanghai team today to discuss your project and receive expert support for injection mold manufacturing and plastic injection molding production.


Professional Insert Molding Services in China

 Insert molding is a plastic injection molding process where a pre-formed component is placed into a mold and plastic is injected around it to create a single integrated part.

At CNMOULDING, we provide high-quality insert molding services in China, helping customers produce strong, reliable, and cost-effective components.

What is Insert Molding?

Insert molding involves placing inserts such as metal components into a mold cavity before injection.

During the process:

  • Inserts are positioned in the mold

  • Molten plastic is injected around them

  • The plastic solidifies, forming a single integrated part

This eliminates the need for secondary assembly.

Advantages of Insert Molding

Insert molding offers key structural benefits:

Strong Mechanical Bonding

Plastic tightly surrounds the insert, creating high strength.

Reduced Assembly Cost

Multiple parts are combined into one, reducing labor.

Improved Product Reliability

Fewer assembly steps mean fewer failure points.

Better Structural Performance

Ideal for components requiring strength and durability.

Applications of Insert Molding

Insert molding is widely used in engineering and industrial applications.

Automotive

  • Electrical connectors

  • Sensor components

  • Threaded parts

Medical Devices

  • Precision instrument components

  • Embedded connectors

Electronics

  • Connectors

  • Cable assemblies

Industrial Products

  • Fasteners

  • Structural plastic parts

Materials Used in Insert Molding

Common materials include:

  • ABS

  • PC

  • Nylon (PA)

  • POM

Insert materials include:

  • Brass

  • Stainless steel

  • Aluminum

Insert Molding vs Overmolding

Insert molding is often confused with overmolding, but they serve different purposes.

 Overmolding is used to combine multiple plastic materials, often for improved grip, sealing, or appearance.

For a full explanation, visit:

Overmolding Process

Our Insert Molding Capabilities

We provide complete insert molding solutions:

  • Insert mold design

  • Precision mold manufacturing

  • Automated insert placement

  • High-volume production

Our team ensures stable production and consistent quality.

Medical Injection Mold

Medical Mold

Medical Mold