2026年4月20日星期一

Plastic Injection Mold Design Guide


Key Principles for High-Quality Injection Mold Manufacturing

Plastic injection mold design is one of the most critical steps in the entire injection molding manufacturing process. A well-designed mold ensures consistent product quality, stable production cycles, and long mold life. Poor mold design, however, can lead to costly defects such as warpage, flash, sink marks, or short shots.

For companies developing plastic products, understanding the fundamentals of plastic injection mold design can help reduce development risks and improve manufacturing efficiency.

At CNMOULDING, a Shanghai-based injection mold manufacturer established in 1997, our engineering team has designed and manufactured hundreds of molds for customers in automotive, medical, electronics, and industrial industries. With more than 25 years of mold manufacturing experience and certifications including ISO9001 and ISO13485, we understand how critical proper mold design is for successful production.

This guide explains the key principles of injection mold design and how manufacturers optimize molds for precision and efficiency.

What Is Plastic Injection Mold Design

Plastic injection mold design refers to the engineering process of creating a mold structure that shapes molten plastic into finished parts during the injection molding process.

A typical injection mold consists of several major components:

  • cavity and core

  • runner system

  • gate system

  • cooling channels

  • ejector system

  • mold base structure

Each component must be carefully designed to ensure smooth plastic flow, proper cooling, and reliable part ejection.

Even small design errors can lead to production defects or inefficient manufacturing cycles.

Key Factors in Injection Mold Design

Several engineering factors must be considered when designing a plastic injection mold.

Part Geometry

The geometry of the plastic part has the greatest impact on mold design.

Designers must consider:

  • wall thickness

  • ribs and bosses

  • undercuts

  • draft angles

Complex part geometry may require additional mold mechanisms such as sliders or lifters.

Proper design optimization at this stage helps avoid unnecessary mold complexity and reduces tooling cost.

Wall Thickness

Uniform wall thickness is essential for high-quality molded parts.

If the wall thickness varies significantly across the part, the plastic may cool unevenly, which can cause:

Most plastic parts are designed with wall thickness between 1.5 mm and 3 mm, depending on the material and application.

Maintaining consistent thickness helps improve molding stability and reduce cycle time.
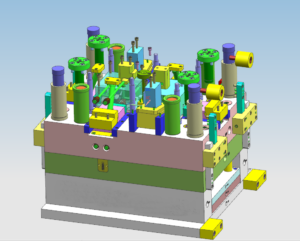
Mold design

Mold design

Draft Angles

Draft angles allow molded parts to be easily ejected from the mold cavity.

Without sufficient draft, parts may stick to the mold, leading to surface damage or production interruptions.

Typical draft angle guidelines include:

  • 1°–2° for smooth surfaces

  • 2°–3° for textured surfaces

Proper draft design improves production efficiency and extends mold life.

Gate Design

The gate is the entry point where molten plastic flows into the mold cavity.

Gate design directly affects:

  • filling balance

  • part appearance

  • internal stress

Common gate types include:

  • edge gate

  • pin gate

  • submarine gate

  • hot runner gate

Selecting the correct gate type helps ensure stable filling and high-quality molded parts.
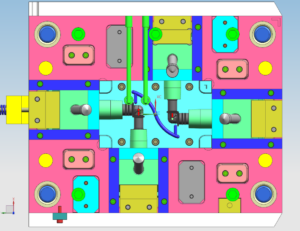
Plastic Injection Mold Design

Plastic Injection Mold Design

Cooling System Design

Cooling channels are responsible for removing heat from the molten plastic after injection.

Efficient cooling design is essential because cooling accounts for more than 60% of the injection molding cycle time.

A well-designed cooling system provides:

  • uniform temperature distribution

  • shorter cycle times

  • reduced part deformation

Advanced mold manufacturers often use Moldflow simulation to optimize cooling channel placement.

Real Case Study: Consumer Electronics Housing Mold

A European consumer electronics company contacted our engineering team in Shanghai to develop an injection mold for a smart device housing.

Project Details

Material: ABS
Part size: 180 mm enclosure
Production volume: 500,000 units per year

Initial Design Challenges

The original product design contained several thick rib structures and uneven wall thickness. During simulation analysis, these features were predicted to cause significant sink marks and potential warpage.

If the mold had been manufactured directly from this design, production stability would likely have been compromised.

Engineering Optimization

Our design engineers conducted a DFM (Design for Manufacturing) analysis and proposed several improvements:

  • optimized rib thickness

  • adjusted wall thickness distribution

  • redesigned gate location

Moldflow simulation was used to verify the improved design before mold manufacturing.

Final Results

After design optimization:

  • sink mark defects were eliminated

  • mold cycle time was reduced

  • production stability improved significantly

The customer successfully launched the product and achieved reliable mass production.

This case demonstrates how proper injection mold design can significantly improve manufacturing performance.

Common Injection Mold Design Mistakes

During product development, several design mistakes often lead to molding problems.

Common issues include:

Uneven Wall Thickness

Leads to warpage and sink marks.

Insufficient Draft Angles

Causes parts to stick inside the mold.

Poor Gate Location

Results in incomplete filling or cosmetic defects.

Inadequate Cooling Design

Leads to longer cycle times and part deformation.

Working with experienced mold designers can help avoid these issues early in the development process.

Why Experienced Mold Design Matters

Injection mold design requires deep knowledge of both plastic materials and manufacturing processes.

At CNMOULDING, our engineering team evaluates each project based on:

  • product geometry

  • material properties

  • production volume

  • mold life requirements

Our factory in Shanghai provides complete services including:

  • injection mold design

  • mold manufacturing

  • plastic injection molding production

  • quality inspection and testing

With over 25 years of experience and certifications including ISO9001 and ISO13485, we support customers worldwide with reliable mold manufacturing solutions.

Start Your Injection Mold Project

If you are developing a new plastic product and need professional support for plastic injection mold design, our engineering team can help review your design and recommend the most efficient manufacturing solution.

Contact our Shanghai team today to discuss your project and receive expert assistance for mold design and injection molding production.

2026年4月12日星期日

Injection Molding Flash: Causes, Prevention, and Real Manufacturing Solutions

 Flash is one of the most common quality defects in plastic injection molding production. It appears as a thin layer of excess plastic that leaks out of the mold cavity and forms along the edges or parting lines of a molded part.

While flash may seem like a minor cosmetic issue, it can cause serious problems in manufacturing. Excess flash often requires additional trimming operations, increases production costs, and in some industries—such as medical devices or precision electronics—it can lead to complete product rejection.

At CNMOULDING (Shanghai), a plastic injection mold manufacturer established in 1997, we frequently help customers troubleshoot injection molding defects during product development and mass production. With over 25 years of experience in mold manufacturing and injection molding services, our engineering team has solved many flash-related issues across industries including automotive, medical, and consumer electronics.

In this article, we explain what injection molding flash is, why it occurs, and how manufacturers can prevent it, along with a real case study from our factory.

What Is Flash in Injection Molding

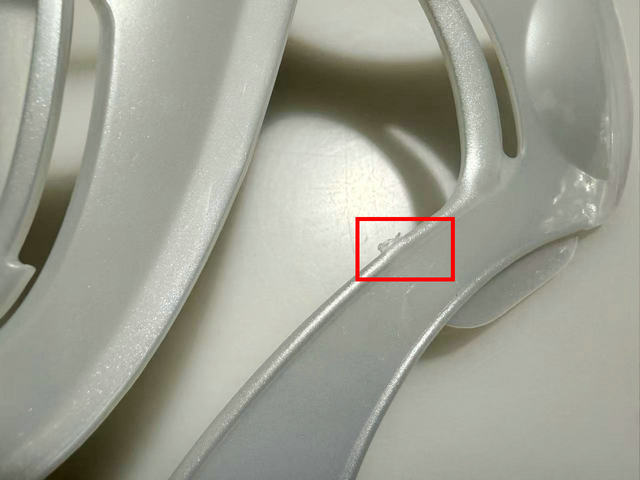
Injection Molding Flash

Injection Molding Flash

Flash occurs when molten plastic escapes from the mold cavity during the injection process and solidifies outside the intended part geometry.

It typically appears in areas such as:

  • the mold parting line

  • ejector pin locations

  • slider interfaces

  • venting areas

Flash may appear as a thin plastic film that extends beyond the edges of the molded part.

In high-volume production environments, even small amounts of flash can cause significant manufacturing challenges, including:

  • increased manual trimming operations

  • poor product appearance

  • assembly interference

  • higher scrap rates

For precision products, preventing flash is essential to maintaining consistent product quality.

Why Flash Happens in Injection Molding

Flash can be caused by several factors related to mold design, processing parameters, and machine performance.

Understanding the root cause is the first step in solving the problem.

1 Insufficient Clamping Force

During injection molding, the mold must remain tightly closed while molten plastic is injected under high pressure.

If the injection pressure exceeds the machine’s clamping force, the mold halves may separate slightly. Even a microscopic gap can allow molten plastic to escape, creating flash.

Solution

The injection molding machine must provide sufficient clamping force to keep the mold completely closed during the injection stage.

Engineers typically verify the clamping force requirement during mold design to ensure the selected machine can handle the injection pressure.

2 Worn Mold Parting Surfaces

Over time, mold components may experience wear due to repeated production cycles.

If the parting surfaces of the mold become worn or damaged, gaps may form between the mold halves.

These gaps allow molten plastic to leak out during injection.

Solution

Regular mold maintenance is essential to prevent flash caused by wear. In high-volume production molds, parting surfaces should be inspected and polished periodically.

Using high-quality mold steel can also extend mold life and reduce wear.

3 Excessive Injection Pressure

While high injection pressure can improve cavity filling, excessive pressure may force molten plastic into small gaps within the mold.

This can cause flash to appear along the parting line or around ejector pins.

Solution

Optimizing injection parameters—such as injection pressure, injection speed, and holding pressure—can reduce the risk of flash.

Balancing these parameters helps ensure the cavity is filled without overpacking the mold.

4 Poor Mold Design or Venting

Improper mold design can also contribute to flash defects.

If venting grooves are too large or if the mold parting surfaces are not properly aligned, plastic may leak out during the injection process.

Solution

Proper mold design is critical for preventing flash.

At CNMOULDING, our engineering team conducts DFM (Design for Manufacturing) analysis and Moldflow simulation to identify potential molding issues before the mold is manufactured.

Real Case Study: Medical Device Housing

A medical device manufacturer from Europe approached us with a quality problem involving flash on a plastic diagnostic device housing.

Because the product was used in a healthcare environment, strict cosmetic and dimensional requirements applied.

Project Details

Material: medical-grade PC
Part type: diagnostic device housing
Production volume: 600,000 parts per year

Problem Description

During production, visible flash appeared along the parting line of the molded parts.

Although the flash thickness was small, it interfered with the assembly of internal components.

Manual trimming was required, which increased production cost and slowed manufacturing.

Engineering Analysis

Our Shanghai engineering team performed a detailed analysis of the molding process.

The investigation revealed two main issues:

  1. The mold parting surface had minor wear after extended production cycles.

  2. Injection pressure settings were higher than necessary for the material and part geometry.

These factors allowed molten plastic to escape from the mold cavity.

Engineering Solution

To solve the flash issue, several improvements were implemented.

1 Mold Surface Reconditioning

The mold parting surfaces were re-polished to restore perfect alignment and eliminate micro gaps.

2 Injection Parameter Optimization

The molding process parameters were optimized, including:

  • reducing injection pressure

  • adjusting holding pressure

  • refining injection speed

3 Clamp Force Adjustment

The machine clamping force was slightly increased to ensure stable mold closure.

Final Results

After these improvements, the production results were significantly improved.

  • flash defects reduced by over 95%

  • manual trimming eliminated

  • production efficiency increased

The customer successfully resumed full production, and the product passed all quality inspections under ISO13485 medical manufacturing standards.

Best Practices to Prevent Flash in Injection Molding

Preventing flash requires a combination of proper mold design, machine selection, and process control.

Key recommendations include:

Use Adequate Clamping Force

Ensure the injection molding machine has sufficient clamp force to handle the required injection pressure.

Maintain Mold Surfaces

Regular mold maintenance prevents wear that can create gaps between mold components.

Optimize Injection Parameters

Balanced injection pressure and holding pressure help prevent excessive material flow outside the cavity.

Perform Moldflow Simulation

Simulation analysis helps identify potential molding issues before mold manufacturing begins.

Why Experience Matters in Mold Manufacturing

Injection molding defects such as flash often require experienced engineers to identify the true root cause.

At CNMOULDING (Shanghai), we combine:

  • over 25 years of injection mold manufacturing experience

  • advanced mold design technology

  • precision machining equipment

  • strict quality control systems

Our factory operates under ISO9001 quality management standards and ISO13485 certification for medical device manufacturing, ensuring reliable production for demanding industries.

Need Help Solving Injection Molding Defects?

If your project is experiencing flash defects, short shots, sink marks, or warpage issues, our engineering team can help analyze the problem and provide effective solutions.

CNMOULDING specializes in:

  • precision injection mold manufacturing

  • plastic injection molding production

  • mold design optimization

  • manufacturing troubleshooting

Contact our Shanghai engineering team today to discuss your project and receive professional support.

Injection Molding Material Selection Guide


How to Choose the Right Plastic Material for Your Project


Reduce Risk. Control Cost. Ensure Manufacturability.

Why Material Selection Is Critical

Choosing the wrong material can cause:

  • Product failure or deformation
  • Poor surface finish
  • Assembly issues in multi-material parts
  • Increased production cost
  • Mold redesign and delays

In injection molding, material selection directly impacts cost, quality, and production success

Step-by-Step Material Selection Process

Step 1: Define Functional Requirements

Ask:

  • Does the part need high strength?
  • Will it face impact or stress?
  • Is flexibility required?

Examples:

  • Structural parts → Nylon (PA), PC
  • Flexible parts → PP, TPE

Step 2: Consider Operating Environment

  • High temperature?
  • Chemical exposure?
  • Outdoor use (UV)?

Examples:

  • High heat → PC, Nylon
  • Chemical resistance → PP, PE

Step 3: Evaluate Surface & Appearance

  • Transparent or opaque?
  • Glossy or textured?
  • Color requirements?

Examples:

  • Transparent parts → PC
  • Cosmetic parts → ABS

Step 4: Check Manufacturing Compatibility

Material must match the process:

  • Shrinkage behavior
  • Flowability
  • Cooling characteristics

Poor selection = warpage, defects, low yield

Step 5: Consider Production Volume & Cost

  • High volume → optimize material + cycle time
  • Low volume → flexibility matters

 Material cost ≠ total cost
Processing cost is equally important

Material Selection vs Manufacturing Process

Material choice often determines the manufacturing method.

Multi-Material Products

If your design requires:

  • Soft-touch + rigid structure
  • Sealing features
  • Multi-layer materials

Overmolding
https://www.injectionmoldchina.com/overmolding/

2K Injection Molding
https://www.injectionmoldchina.com/2k-injection-molding-automotive/

Metal + Plastic Integration

If your design includes:

  • Metal inserts
  • Threaded components
  • Reinforcement structures

You may need:

Insert Molding
https://www.injectionmoldchina.com/insert-molding/

Choosing the wrong process at this stage can increase cost by 30%+

Quick Material Selection Guide

RequirementRecommended Material
High strengthNylon (PA), PC
Impact resistanceABS, PC
Chemical resistancePP, PE
TransparencyPC
Low frictionPOM
Soft touchTPE / TPU

Common Mistakes Engineers Make

  • Selecting material based only on price
  • Ignoring shrinkage and tolerance
  • Choosing incompatible materials for multi-shot molding
  • Not considering mold design impact

These mistakes often lead to redesign, delays, and higher costs

 How We Help

We don’t just supply materials — we provide engineering solutions:

 Material Recommendation

Based on function, cost, and manufacturability

DFM Analysis

Optimize part design for injection molding

Process Matching

Overmolding, 2K, or Insert Molding selection

Cost Optimization

Reduce material waste and cycle time

Get Free Material Selection Support

Not sure which material is right?

Send us your design files or requirements.

You will receive:

  • Material recommendation
  • Manufacturing process suggestion
  • Cost optimization advice

Start Your Project

Upload your 3D files and get expert feedback within 24 hours

Upload Your Design Now

Related Solutions

To achieve the best results, material selection often works together with:

Final Insight

The right material choice can reduce total production cost by 20–50% and prevent costly redesigns.

Get it right before tooling starts